If you’ve ever spent time around a precision centerless grinder, you know the biggest headache isn’t the grinding wheel or the coolant—it’s keeping the workpiece perfectly concentric. For those who don’t know, concentricity here means the outer surface of your part lines up dead-center with its inner bore or axis. Mess that up, and you’re left with parts that wobble, vibrate, and get rejected faster than you can hit the emergency stop. As someone who’s been selling and troubleshooting these grinders for over a decade, I’ve seen every trick in the book—plus a few that actually work, and a bunch that don’t. Today I’m breaking down exactly how to nail concentricity every single time on your centerless grinder. Precision Centerless Grinder

First, let’s get one thing straight: centerless grinding doesn’t use chucks or collets like other grinders. The part sits between two wheels: the grinding wheel that does the cutting, and the regulating wheel that spins the part at the right speed. There’s also a work blade that supports the whole thing. So all your concentricity issues trace back to one of these three parts, or how you set them up. No exceptions.
Let’s start with the work blade—this is the unsung hero. I see so many shops skip basic blade maintenance, and that’s where concentricity dies. Think of the work blade as the foundation of your setup. If it’s worn, chipped, or even just a little off-kilter, the part will rock as it feeds through, throwing the axis way off. A few months ago, a regular customer called me panicking because their pins kept coming out with 0.005mm of runout. When I showed up, their work blade was pitted from 6 months of grinding hardened steel. We replaced it, trued the blade, and fixed the runout in 10 minutes.
So how do you do it right? First, always use a blade made for your workpiece material. Soft blades for aluminum won’t hold their shape long, and steel blades for carbide will chew up the part. Second, check the blade height. This is a common mistake that new operators make. The ideal blade height is such that the center of the workpiece is about 1/3 of its diameter above the line connecting the grinding wheel center and the regulating wheel center. Too low, and the part will dig into the blade, causing friction that makes it wander. Too high, and you risk the part lifting out of the setup—ask me how I know that last one. If you’re not sure, use a height gauge or a simple dial indicator to double-check.
Next up: the regulating wheel. This wheel controls the part’s speed and rotation, so if it’s not trued properly, your concentricity is done before you even start. I can’t tell you how many times an operator will grind for hours, run a part, see runout, and blame every part in the shop except the regulating wheel. Tiring a regulating wheel is non-negotiable, and it needs to be done regularly—not just when the surface looks rough. When you true it, use a diamond dresser that’s sharp, and feed it slowly. If you rush the truing, you’ll get chatter marks on the wheel, which transfer right to the part. Also, make sure the regulating wheel’s axis is parallel to the grinding wheel’s. Even a 0.001mm difference will throw the part off. Most modern centerless grinders have adjustable wheels, so take 5 minutes to dial in that parallelism with a test bar before you start production.
Wait, another thing about the regulating wheel: its hardness. Soft regulating wheels are for soft materials like brass or plastic, because they grip the part better without marring it. Hard regulating wheels are for hardened steel or carbide—they last longer and keep rotation consistent. I once had a customer run a batch of stainless steel pins with a soft regulating wheel, and every single one had concentricity issues. Swapping to a medium-hard wheel fixed it immediately. Don’t just grab the closest wheel—match it to your workpiece.
Now let’s talk about the grinding wheel, even though it’s less directly linked to concentricity than the other two, it still plays a role. If the grinding wheel is out of balance, it will vibrate, and that vibration will make the part wobble. Balancing your grinding wheel every time you mount it is mandatory. I use static balancing for new wheels, but dynamic balancing is even better—especially for high-volume production. A lot of shops skip dynamic balancing, but on parts that require sub-micron concentricity, it’s the difference between good parts and scrap. Also, dress the grinding wheel correctly before you start a new job. A dull grinding wheel will force the part to work harder, leading to inconsistent rotation and thus poor concentricity.
Then there’s the workpiece itself. Wait, the part you’re grinding matters more than you think. If your part has an out-of-round starting shape, no setup is going to fix that. I see this all the time: an operator gets a batch of cast parts that are already oval, puts them on the grinder, and wonders why they come out oval. Before you even load parts into the grinder, check their initial roundness with a dial indicator. If they’re even a little out of round, use a pre-grinding operation to true them up first. For parts with long lengths, like shafts, make sure they’re not bending from their own weight. If a shaft is 300mm long and only supported at the ends, it will sag, leading to concentricity errors in the middle. Some grinders have center supports for long parts—use them. It’s a small step that makes a huge difference.
Feed rate is another often-overlooked factor. If you feed parts through the grinder too fast, the regulating wheel can’t keep up, so the part skids instead of rotating smoothly. Skidding means inconsistent rotation, which kills concentricity. For precision jobs, take your time with the feed rate. Slow and steady is always better when you’re chasing tight tolerances. I usually start with a test part, check its concentricity, and adjust the feed rate until it’s perfect. Don’t be afraid to tweak it—even a 10% change can make a big difference.
Coolant might sound irrelevant, but hear me out. If your coolant is dirty or not delivered at the right pressure, it can cause thermal expansion of the part. Even a tiny amount of expansion will throw off concentricity, especially on small parts or materials that heat up easily, like aluminum. Make sure your coolant system is filtered regularly, and that the pressure is set correctly—not too high (it can wash away the part) and not too low (it won’t cool enough). I always tell customers to run coolant through the grinder for 5 minutes before starting production to make sure the whole system is stable and at the right temperature.
Now, let’s get to the post-setup check. You can do all the setup in the world, but if you don’t verify, you’ll still get bad parts. Use a dial indicator to check runout on a test part before you run the whole batch. Runout is basically how much the part wobbles, and it’s directly linked to concentricity. For example, if you need concentricity within 0.002mm, your runout on the test part should be less than that. If it’s not, don’t just adjust one thing—check all the variables: blade height, wheel trueness, wheel balance, feed rate. I once had a job where runout was off, and I spent 20 minutes adjusting the blade, only to realize the regulating wheel wasn’t parallel. Don’t jump to conclusions—systematically check each part.
Another pro tip: consistent part loading. If you load parts at different angles into the grinder, you’ll get inconsistent rotation, leading to poor concentricity. Most modern centerless grinders have automated feeders, but if you’re loading manually, use a jig to make sure each part is positioned the same way every time. Even a tiny angle difference can add up when you’re dealing with tight tolerances.
Wait, let’s address a common myth: some operators think that higher precision grinders don’t need as much setup. That’s half true—high-quality grinders (like the ones we supply) have better built-in alignment, but they still need proper setup to hit their maximum precision. A $500k grinder set up wrong will make the same bad parts as a $50k grinder set up right. Don’t rely on the machine to fix your setup mistakes.
Let’s put this all together with an example. Last year, a customer was running small ferrules for medical devices, needing concentricity within 0.001mm. They were getting 0.003mm runout, and tried 3 different grinders before calling us. We walked through their setup: their work blade was worn, regulating wheel wasn’t trued, and they were feeding parts too fast. We replaced the blade, trued both wheels, balanced the grinding wheel, and adjusted the feed rate. The first test part came in at 0.0008mm runout—perfect, right in spec. They ended up ordering two more grinders after that.
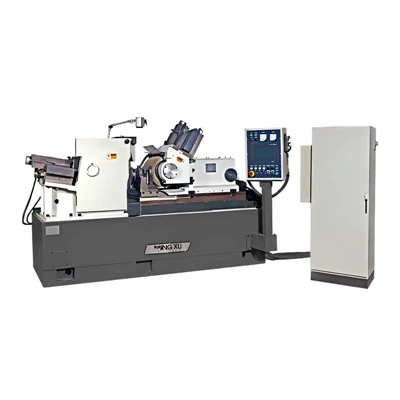
Now, if you’re struggling with concentricity on your centerless grinder, don’t guess. Go back to the basics: check your work blade, true your wheels, balance, slow down the feed, and test with parts. And if you’re looking to upgrade your grinder or get expert support, we’re here to help with all your precision centerless grinding needs. Reach out to discuss your specific application and find the right solution for your parts.
Precision Centerless Grinder References: 1. Stephenson, D. A., & Agapiou, J. S. (2016). Metal Cutting Theory and Practice. CRC Press. 2. Tonshoff, H. K., Brinksmeier, E., & Wennerberg, J. (1992). Centerless Grinding: Theory and Practice. CIRP Annals. 3. Webster, J., & Mindek, R. (2000). Grinding Wheels: Technology and Performance. Marcel Dekker.
Wuxi Mingxu Machinery Equipment Co., Ltd.
As one of the most professional precision centerless grinder manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to buy the best precision centerless grinder for sale here from our factory. Also, custom service is available.
Address: No. 5-5 Jinke Wealth Plaza, Changjiang North Road, Xinwu District, Wuxi City, Jiangsu Province
E-mail: yingyingmxjd@163.com
WebSite: https://www.mingxu-china.com/
